Your Cart is Empty

Constraint-Aware Sheet Metal Flattening: Embedding Manufacturing Logic into CAD-to-CAM Workflows
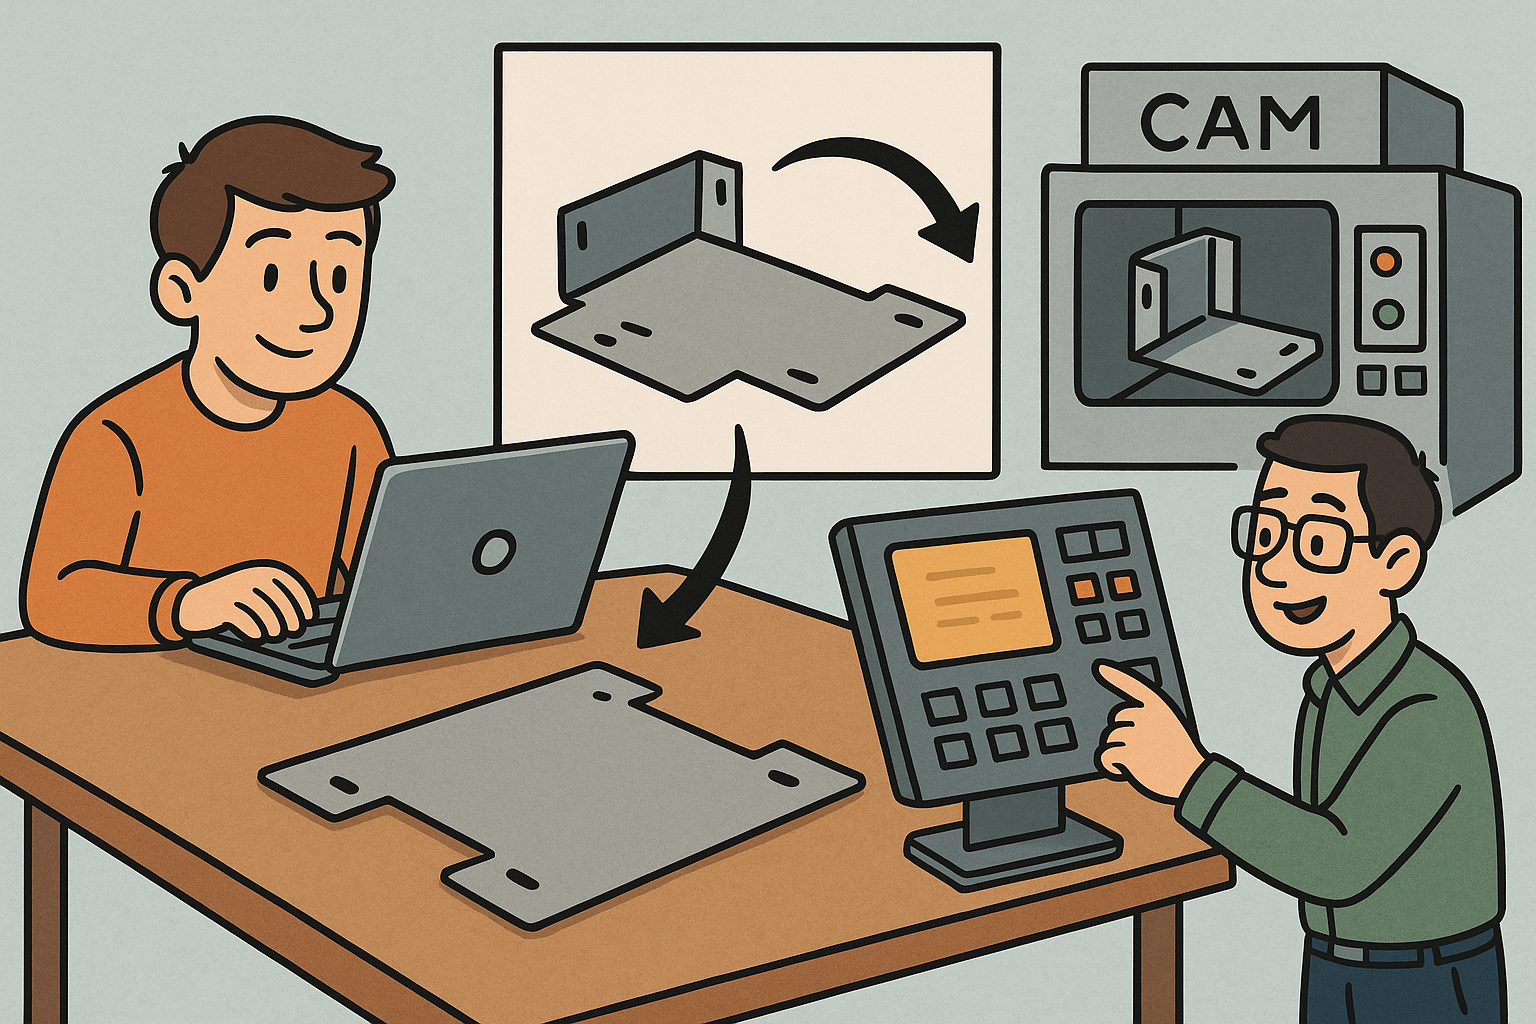


Sheet metal design rarely fails on geometry; it fails when geometry ignores production. The shortest route to predictable schedules, accurate quotes, and clean first articles is to make manufacturing logic explicit in the software that flattens parts. By treating flattening as a decision system rather than a one-click unfold, teams can encode the quirks of materials, machines, and methods directly into the model. That means a designer adjusting a flange length instantly sees whether the part will air-bend correctly in a 12 mm V-die, whether the grain flows along the long axis, and whether that obround relief matches available punches. This approach avoids late-stage redraws and emailed markups, replacing them with a tight loop of embedded guidelines, repeatable outputs, and auditable rationale. In practice, it means carrying the reality of bend radii, springback, and minimum distances with the part from CAD to CAM and onto the press brake. The payoff is substantial: fewer reworks, shorter RFQ cycles, and more confidence in supplier handoffs, all anchored by a living thread of data connecting design intent to shop-floor outcomes.
Why automate sheet metal flattening with manufacturing constraints
Bridging ideal geometry and shop-floor reality
Unfolding a part that ignores production constraints is a promise the shop cannot keep. Automated flattening should therefore embed the realities that operators manage every shift. These realities include the interplay of material thickness, target radius, and selected die opening; the way the neutral axis shifts per alloy and temper; and the stubborn behavior of springback under different angles. A robust system treats these not as post-hoc annotations but as first-class constraints that shape the flat. Practical automation translates geometric intent into a manufacturable pattern while preserving the functional intent of the 3D design. That means calculating bend lengths from a configurable K-factor or table, honoring grain direction for cosmetic panels, and catching violations like holes creeping too close to bends. It also means offering predictable reliefs and notches that match stocked tooling. To ground the transformation, the software should surface the trade-offs explicitly, so a designer can choose between a slightly larger inside radius for die availability or a different bend sequence that avoids interference without adding seams.
- Bend radii linked to die openings and thickness
- Neutral axis shifts via K-factor or standards (e.g., DIN 6935)
- Grain orientation constraints for cosmetics and forming
- Tooling limits and minimum feature distances
- Expected springback and achievable angles
DFM rules and codified consistency to reduce rework
Most rework stems from naïve unfolds that miss fundamentals of design for manufacturability. Embedding DFM logic directly in the flattening step shrinks that gap. A rules engine can enforce a minimum flange length for clamping, validate hole-to-bend offsets to avoid distorting pierce holes, and insist on reliefs when approaching a corner. These checks should not merely flag issues; they should auto-size and style features to match the punches and notching options the shop actually stocks. Consistency emerges when reliefs, notches, and hems follow a shared library, and the system explains why a given choice was made. This makes the decisions auditable across teams and suppliers, and it removes personal style drift from critical features. The result: fewer hand-edited DXFs, fewer surprise burrs at tight corners, and a flatter learning curve for new designers because the software enforces the “house way” of flattening. With every accepted fix, the knowledge base grows and future parts benefit automatically.
- Minimum flange length and backgauge access
- Hole-to-bend and slot offsets with automatic adjustments
- Relief requirements (rectangular, obround, tear) with punch matching
- Standardized notch geometries and hem/curl templates
- Company rule packs aligned to ISO/DIN and material libraries
Speeding quotes, CAM, and concurrent design decisions
When flats arrive already aligned with press-brake, turret, and laser capabilities, quoting and CAM accelerate dramatically. Generating flat patterns with bend notes, PMI, grain arrows, and operation tags eliminates downstream rework and gives estimators reliable cycle times. In parallel, a live manufacturability engine inside CAD supports concurrent design: as parameters change, the system re-unfolds with current constraints, preventing late-stage redraws and cascading drawing updates. The faster that feedback loop runs, the fewer times a team commits to a geometry that cannot survive the brake. By emitting consistent bend lines, directions, and angle/radius notes tied to known die sets, CAM can autopopulate tools and sequences, while buyers see realistic press time in RFQs. Over time, these outcomes compound; suppliers receive uniform data, internal teams share a single source of forming truth, and planning assumptions stop drifting. The net effect is higher quote win rates and fewer surprises at first article, enabling designers to move forward with confidence instead of hedging around uncertainty.
- PMI-rich outputs for downstream CAM and inspection
- Instant manufacturability feedback while editing CAD
- Supplier-ready data that reduces clarification cycles
- Predictable press-brake time estimates tied to tooling
- Consistent standards reduce onboarding friction
Core algorithms and representational choices
Feature graph extraction
The foundation of constraint-aware flattening is a reliable representation of the part’s forming intent. Instead of treating the model as undifferentiated faces and edges, the system should extract a feature graph that identifies bends, hems, curls, dimples, beads, louvers, and locking seams, and distinguishes developable walls from formed regions. Each feature becomes a node carrying thickness, inside radius, bend angle, relief state, and candidate tooling. Edges encode adjacency and dependency: which flanges share a corner, which bends chain into a sequence, and where a louver interrupts an otherwise developable panel. A bend graph captures the ordering options and feasible interactions, enabling algorithms to test sequences for interference and to select relief strategies that keep corner behavior clean. With this structured view, the software can reason upstream and downstream: if a hem requires a different die, the graph indicates whether that choice forces a prior bend to flip orientation. Crucially, the graph survives edits so propagation is incremental rather than a full rediscovery, keeping interactivity high.
- Nodes: bend, hem/curl, bead, louver, jog, seam
- Attributes: angle, radius, thickness, relief type, tooling candidates
- Edges: adjacency, co-linear chains, corner sharing, forming precedence
- Scopes: developable vs. formed zones for flattening eligibility
- Incrementality: fast updates under parameter changes
Developability detection and segmentation
A robust system must spot where geometry cannot flatten without stretching. Drawn embosses, deep dimples, and beads introduce local strain that simple developable mappings cannot absorb. The algorithm should detect such non-developable patches and either route them to secondary forming operations or apply compensated approximations with explicit warnings. Segmentation carves the model into panels that are flattened with confidence and zones that will be formed post-cut. At panel boundaries and corners, the software auto-inserts reliefs sized to material and punch availability, selecting rectangular, obround, or tear styles as appropriate. In tight corner clusters, corner reliefs prevent “knife edges” and slivers. These insertions are constraint-driven: minimum web width, minimum distance to piercing, and grain-sensitive notch orientations are all validated and updated as thickness or angle changes. By formalizing segmentation, the system stops designers from relying on guesswork and makes the plan explicit: where to laser-cut, where to press, and where to add a secondary hit.
- Detect drawn features and stretch zones from curvature and thickness cues
- Isolate formed regions as secondary operations
- Auto-size bend and corner reliefs that match stocked punches
- Preserve minimum web widths and hole offsets at corners
- Flag approximations when compensations exceed thresholds
Neutral axis modeling and flat length prediction
Flat length accuracy decides whether bends meet, gaps close, and holes align after forming. The heart of that accuracy is a defensible model of the neutral axis and bend allowance. Systems should support multiple models—K-factor curves by material and temper, standard tables such as DIN 6935, and air-bend formulas tied to V-die opening and inside radius. For shops with data history, data-driven regressors can outperform generic rules, especially when they incorporate angle-dependent springback. The solver must also handle multi-radius bends, offset jogs, and chained bends where tolerances accumulate. It should track the effect of shimming, die swaps, and compound sequences without assuming station independence. Tolerance propagation is essential: the flat carries nominal and limits for each segment so that inspection knows where deviations are absorbed. A modern approach treats neutral axis position as a parameterized function of thickness, die, material, and angle, with overrides allowed per bend, turning the flattening engine into a faithful predictor rather than a rough estimate.
- Configurable: K-factor, DIN 6935 tables, and air-bend formulas
- Hybrid models with learned corrections from shop data
- Support for multi-radius and jog features
- Cumulative tolerance tracking across bend chains
- Bend-level overrides with auditable rationale
Constraint-aware unfolding and multi-objective optimization
Unfolding must balance several objectives at once, not merely minimize distortion. A multi-objective optimizer evaluates candidate flattenings to minimize changes to seam counts, preserve the specified grain orientation, satisfy minimum flange and relief constraints, and avoid warping critical features like slots or louvers. The algorithm should consider bend order impacts on GD&T, because the direction and precedence of bends affect datum relationships and resultant tolerances. Rather than a single deterministic route, the system can run a fast search over bend orders admissible by the feature graph, scoring each plan for interference risk and tolerance growth. This approach makes the trade-offs visible: perhaps preserving grain requires rotating the flat in nesting, increasing scrap; perhaps avoiding a louver warp requires a different relief. By propagating PMI and GD&T from 3D to flat, including bend direction arrows and K-factor references, downstream stakeholders inherit the decisions that underpin the geometry, not just polylines. The outcome is a flat that reads like a plan, not a hope.
- Objective terms: seams, grain, feature warping, relief compliance
- Constraints: minimum distances, tool-specific radii, stock sizes
- GD&T propagation with bend order awareness
- Search over admissible sequences for collision safety
- Scorecards that explain chosen unfolding rationale
Robust geometry operations for edge cases
Sheet metal features stress numerical geometry kernels. Small radii at shallow angles create near-parallel faces and “sliver” edges that break Boolean operations. Hems and curls introduce partial-thickness and self-contact scenarios easy to mishandle. A production-ready kernel must use exact or interval arithmetic for stability, alongside tolerant topology that merges microscopic edges below meaningful manufacturing thresholds. Parametric templates for hems, curls, and jogs should be generated with safeguards that reject non-manufacturable inputs before they poison the model. When two reliefs overlap or a hem meets a bend, the engine should enforce manufacturability gates that snap geometry to nearest safe values and document the adjustment. These defenses preserve downstream CAM sanity: laser paths remain clean, bend lines remain continuous, and offsetting does not create zero-length segments. By coupling numerical care with domain-specific templates, the system respects both mathematical and shop constraints, ensuring that “robustness” means parts unfold and cut without 3 a.m. operator heroics.
- Exact/interval arithmetic for small-angle stability
- Tolerant topology to prevent sliver edges
- Parametric templates for hems, curls, and partial-thickness features
- Manufacturability gates with clear diagnostics
- Self-interference detection and safe resolution
From flat pattern to press brake: closing the loop
Tooling selection and press-brake sequencing integration
The flattening engine should not guess at tooling; it should select it. After mapping each bend to feasible dies and punches based on thickness, angle, and inside radius, the system picks a V-die opening and punch that meet both design targets and shop constraints. With tooling fixed, it can simulate press-brake sequencing to test backgauge access, finger positions, and part self-interference across the sequence. Sequencing is not merely about collision avoidance; it also affects achievable tolerances and whether certain bends need flipping. By closing this loop before finalizing the flat, the exported pattern carries meaningful bend notes that match actual stations, saving time on the floor. When the shop revises the plan—for instance, swapping to a different die opening—the model can revalidate bend allowances and update notes, keeping the digital thread intact. This integration transforms flats from generic outlines into executable plans tuned to the cell’s inventory and limitations.
- Auto-selection of die openings and punches from inventory
- Simulation of collisions, backgauge access, and part flips
- Station-aware bend notes aligned with the chosen sequence
- Feedback loop to recompute allowances on tooling changes
- What-if comparisons across alternative sequences
Springback modeling and adaptive compensation
Accurate angle control demands more than a static lookup. A hybrid approach blends analytical estimators with calibrated FEM or surrogate ML models conditioned on material, thickness, angle, and die geometry. The analytical side provides physics-grounded baselines; the ML surrogate fills in nonlinearities unique to a shop’s material lots and machine behavior. The system should employ active learning: ingest measured angles and leg lengths from the press, compare them to predictions, and update K-factors and compensation curves automatically. Each bend becomes a data point that tunes future bends, closing the loop without lengthy manual calibration runs. In practice, this means the same nominal flat cuts today and next quarter will produce consistent results, even as coil properties drift. Where outliers occur, the software flags which inputs (e.g., angle, die opening, alloy lot) most influenced the deviation, keeping the model explainable. Compensation then becomes a living artifact rather than a static table taped to a machine.
- Analytical baselines augmented by shop-trained surrogates
- Die- and angle-dependent springback corrections
- Automatic K-factor updates from measured outcomes
- Explainable features highlight drivers of deviation
- Confidence intervals guiding inspection focus
Standards, data, and interoperability at export
The value of a carefully constrained flat evaporates if the data cannot travel. Exports should include PMI-rich DXF and STEP AP242 with semantic bend lines, directions, angle/radius notes, grain arrows, and operation tags mapped to tooling. Embedding operation metadata enables CAM to auto-assign stations and lasers to interpret micro-joints without tribal knowledge. An automated checker enforces house rules—hole-to-bend distances, tab widths, minimum web sizes—while providing explainable diagnostics with hyperlinks to violating features in the viewer. This makes the rules visible and negotiated, not hidden. MBD-first approaches mean the 3D model remains the authority, with 2D flats derived and traceable, preventing divergence as revisions roll through ECOs. Interoperability also requires versioned material libraries and rule packs so suppliers can match assumptions. The tighter these threads are woven, the fewer email exchanges it takes to clarify intent, and the faster the flat transitions from estimate to cut.
- Annotated AP242 with semantic PMI and bend attributes
- DXF layers for lines, notes, grain direction, and operation tags
- Automated DFM checker with actionable messages
- Versioned material and rules libraries shared with suppliers
- MBD-first hierarchy to keep flats synchronized
Nesting awareness and integrated costing
Flattening cannot ignore nesting. Grain direction, tab placement, and remnant usage all influence sheet utilization and thus cost and carbon. The system should expose nesting constraints upstream: if a panel demands grain parallel to a long flange, the flat should lock a rotation range so CAM and nesting algorithms honor cosmetics and forming anisotropy. Micro-joint/tab placement must respect bend lines and clamp zones, and the flattening engine should propose safe regions for tabs based on the bend graph. As flats aggregate into jobs, the software can surface real-time cost and sustainability estimations tied to utilization, operation counts, and press-brake time. This turns design edits into immediate cost signals: a 2 mm radius increase that unlocks a common die may save minutes per part and allow tighter nests. By treating nesting and costing as first-class citizens, teams avoid local flattening optimizations that lose globally on material yield or takt time.
- Rotation limits and grain orientation preserved for nesting
- Tab/micro-joint guidance that avoids bend lines and clamps
- Remnant-aware constraints to increase yield
- Live cost/carbon updates from utilization and cycle time
- Trade-off visualizations to justify design tweaks
Governance, security, and extensibility
Enterprises need control and customization. Rule packs scoped per supplier let the same design validate differently against in-house brakes versus a high-tonnage partner. A zero-trust posture protects IP by redacting proprietary parameters while still communicating necessary PMI to vendors. Open APIs/Scripts allow teams to encode custom relief shapes, tolerance schemes, and export pipelines, ensuring the tool adapts to the process, not the reverse. Governance also means traceability: who accepted a rule override, which K-factor version computed a bend, and when a material library changed. These audit trails make sign-off defensible and accelerate corrective actions when yields dip. Extensibility ties back to learning: as shops adopt new dies or processes like rotary bending, the software can register those capabilities so future flats consider them. By balancing guardrails with hooks, the system supports craftsmanship without devolving into ad hoc edits that fracture standards.
- Supplier-specific rule packs and capability profiles
- Zero-trust controls for model and PMI sharing
- Scriptable customization for reliefs and tolerances
- Audit logs for overrides, materials, and model versions
- Capability registration to exploit new tools and methods
Conclusion
From geometry to production-ready decisions
Embedding manufacturing constraints into flattening elevates unfolding from a geometric transform to a production decision. The winning stack couples a rich feature graph, a constraint-aware unfolding optimizer, and a feedback loop that learns springback and allowances from real press data. Teams gain fewer reworks because DFM checks and relief insertions happen before flats ever reach CAM. Quotes accelerate as annotated patterns flow with bend notes, grain arrows, and operation tags that mirror actual tooling and sequences. Predictable quality arrives when standards are codified, K-factors are calibrated continuously, and every exported flat tells an unambiguous story an operator can execute. The next chapter extends that loop: live MES feedback closes the gap between plan and outcome; compensation models expand to cover more non-developable forming; and explainable automated checks mature so reviewers can see why a violation matters and how to fix it with one click. This is how every flat becomes “first-article ready”: the right geometry, enriched with the right knowledge, delivered to the right machine, with the confidence that the digital and physical will agree.
Also in Design News